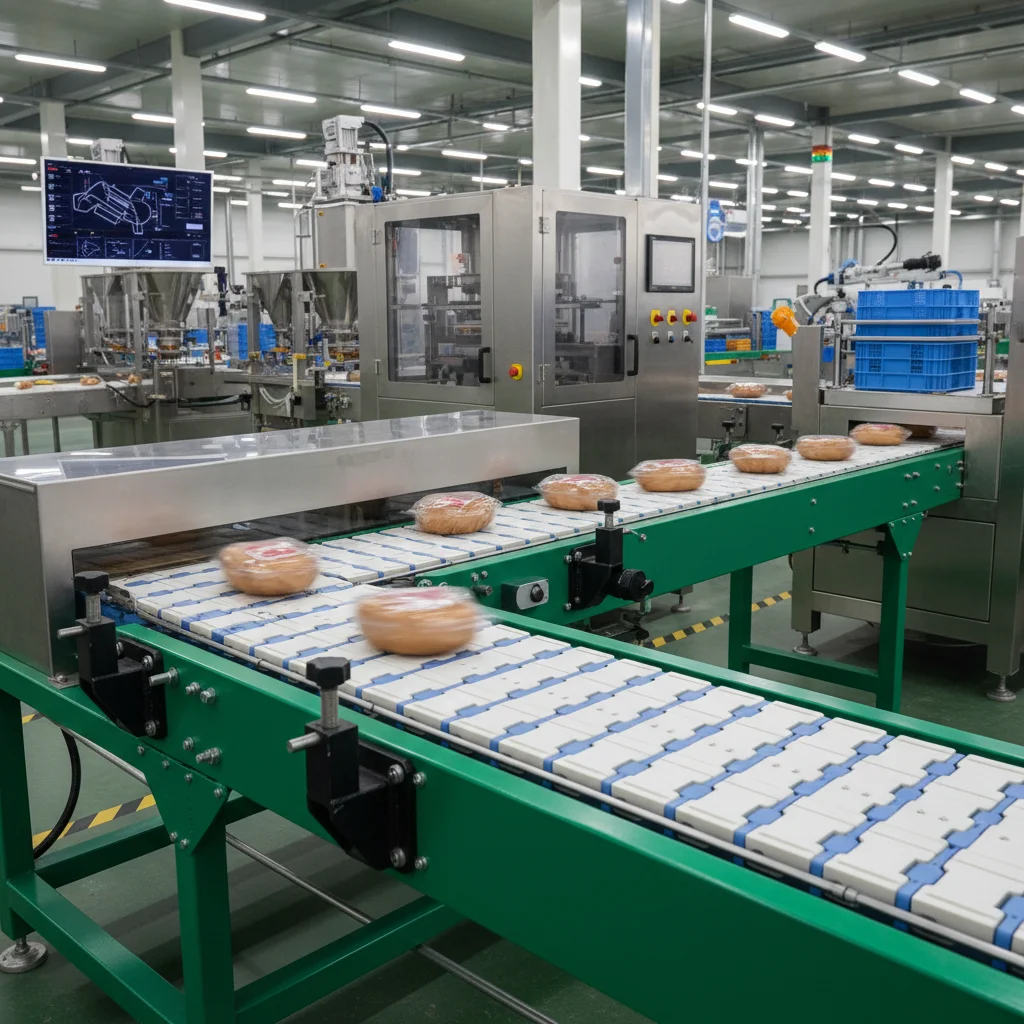
The global demand for high-precision material handling has led to the widespread adoption of the modular conveyor belt, a system designed to replace traditional monolithic belts with interlocking plastic modules. In modern manufacturing, the ability to maintain consistent product flow while minimizing downtime is critical for operational success. These systems provide a scalable and durable alternative that meets the rigorous demands of automated production lines across various sectors.
From a global industry perspective, the shift toward modularity is driven by the need for enhanced hygiene and rapid maintainability. According to international industrial standards, reducing unplanned downtime is one of the most effective ways to increase Overall Equipment Effectiveness (OEE). The modular conveyor belt addresses these challenges by allowing operators to replace damaged sections without dismantling the entire system, ensuring a continuous flow of goods.
Specifically, the 0.5-inch pitch modular belt represents a pinnacle of precision engineering, optimized for the transport of small and delicate items. By utilizing high-grade plastics like Polypropylene (PP), Polyethylene (PE), and Acetal (POM), these systems ensure stability, chemical resistance, and low friction. This makes them an indispensable asset for high-precision industries such as food packaging, pharmaceutical manufacturing, and electronics assembly.

Material Composition and Precision Engineering
The foundation of a high-performance modular conveyor belt lies in its material selection. Utilizing premium industrial-grade plastics such as Polypropylene (PP), Polyethylene (PE), and Acetal (POM), these belts are engineered to withstand extreme environments. These materials provide a critical balance of low friction and high chemical resistance, ensuring that the belt does not degrade when exposed to harsh sanitizing agents or industrial lubricants.
Precision is achieved through advanced injection molding processes. Each module is crafted to maintain a strict 0.5-inch pitch, which is essential for maintaining alignment across the entire system. This level of accuracy prevents the belt from tracking off-center and ensures a smooth transition through sprockets and guide rails, which is vital for transporting delicate components in electronics or pharmaceutical lines.
Key Factors for Operational Stability
Stability in material handling is primarily governed by the pitch and surface properties of the belt. A smaller pitch, such as the 0.5-inch configuration, provides a more continuous support surface, which significantly reduces the risk of small items tipping or slipping during high-speed transport. This precision handling is what allows manufacturers to increase line speeds without compromising product integrity.
Beyond the pitch, the modular linked system offers unmatched structural strength. Unlike fabric belts that can stretch or fray over time, the interlocking plastic modules maintain their geometric integrity under heavy loads. This prevents the "sagging" effect often seen in traditional systems, ensuring that the product remains level as it moves through the production cycle.
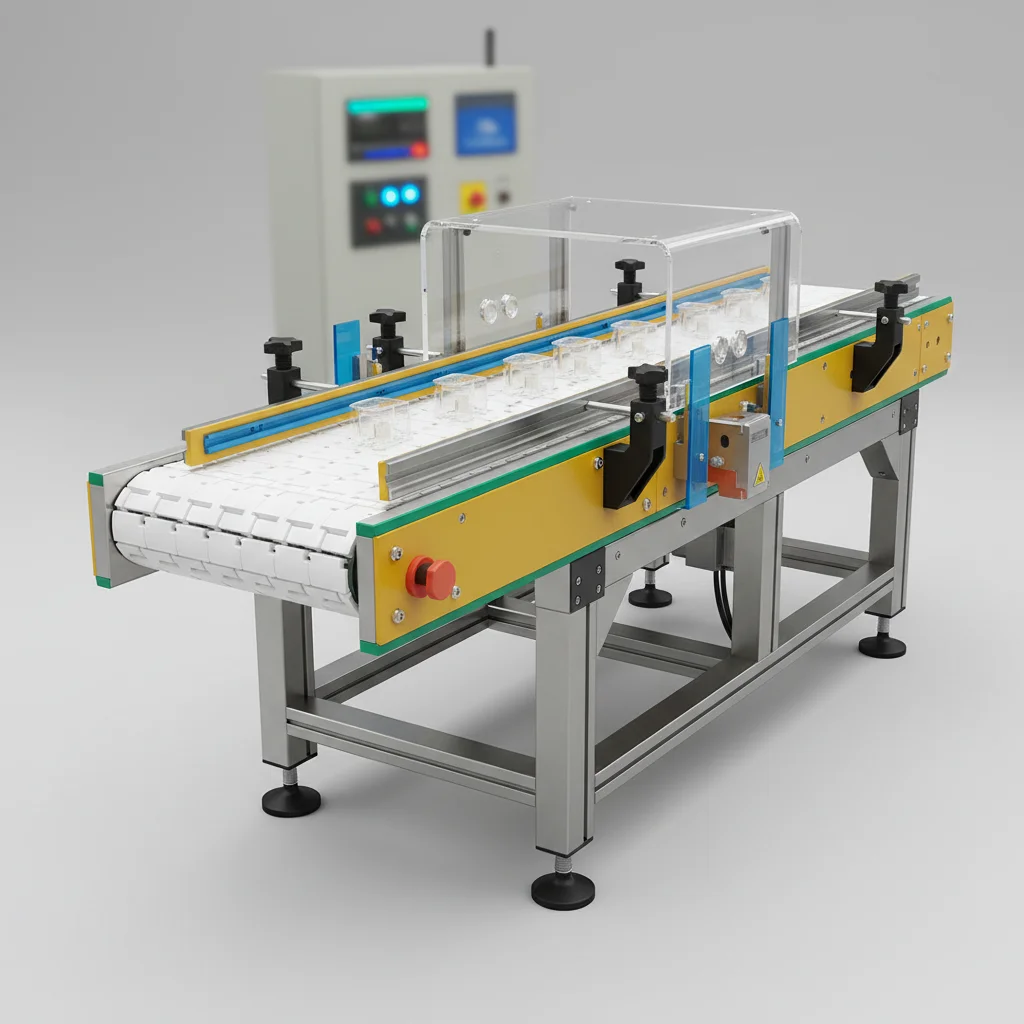
Furthermore, the ability to integrate side guards and guide rails seamlessly into the modular architecture adds another layer of stability. These components work in tandem with the belt's low-friction surface to guide products accurately, making it an ideal solution for complex automated production lines requiring maximum reliability.
Versatility in Industrial Applications
The adaptability of the modular conveyor belt makes it a preferred choice across diverse sectors. In the food and beverage industry, FDA compliance is non-negotiable. The open structure of the modular design allows for efficient drainage and easy cleaning, preventing the buildup of contaminants and ensuring that stringent hygiene standards are met.
In pharmaceutical and electronics assembly, the 0.5-inch pitch is specifically leveraged to handle vials and small capacitors. These high-value items require a stable, vibration-free transit to avoid damage. The precision injection molding of the modular belt ensures a consistent surface that minimizes movement, providing the high-precision handling required for these sensitive industries.
Beyond flat transport, these belts are engineered for geometric flexibility. They can navigate curves, inclines, and declines without compromising the alignment of the payload. This capability allows plant managers to optimize floor space by designing more compact, winding production lines that still maintain high throughput and product stability.
Performance Metrics and Efficiency Analysis
Evaluating the efficiency of a conveyance system involves analyzing throughput, downtime, and maintenance costs. When compared to traditional belt systems, the modular approach demonstrates a significant reduction in "Mean Time to Repair" (MTTR). Because individual modules can be replaced in minutes, the system avoids the hours of downtime associated with splicing or replacing a full-length belt.
The operational efficiency is further enhanced by the low-friction properties of the POM and PE materials. This reduces the energy required to drive the conveyor and minimizes wear on the drive sprockets, leading to a longer overall service life and lower energy costs for the facility.
Efficiency Ratings of Modular Conveyor Belt Configurations
Long-Term Value and Maintenance Benefits
The investment return of a modular conveyor belt is realized through its "renewable" nature. Instead of the entire belt becoming a waste product once a section is worn or damaged, only the affected modules are replaced. This not only lowers the direct replacement cost but also aligns with corporate sustainability goals by reducing industrial plastic waste.
Furthermore, the snap-together assembly method simplifies the installation process. No specialized tools or vulcanizing equipment are needed to expand or modify the belt. This agility allows companies to rapidly reconfigure their production lines to accommodate new product sizes or changes in workflow, providing a strategic advantage in fast-paced markets.
Future Trends in Modular Conveyance
The future of material handling is leaning heavily toward the integration of "smart" components. We are seeing the emergence of modular systems that incorporate embedded sensors for real-time wear tracking. This allows for predictive maintenance, where modules are replaced based on actual wear data rather than a fixed schedule, further optimizing production uptime.
Sustainability is also driving innovation in material science. New bio-based polymers are being developed to offer the same chemical resistance and strength as traditional PP and POM, but with a lower carbon footprint. These "green" modular conveyor belt options will become critical as global regulations on plastic usage tighten.
Finally, the trend toward complete automation (Industry 4.0) requires belts that can integrate perfectly with robotic pick-and-place systems. The high precision of the 0.5-inch pitch provides the exact positioning required for robotic arms to interact with products without error, cementing the role of modular systems in the future of the smart factory.
Comparison of Modular vs Traditional Belts
When deciding between a modular conveyor belt and a traditional belt, the primary consideration should be the cost of downtime. Traditional belts require a full stop and significant labor to replace, often taking hours or days. In contrast, modular systems allow for "on-the-fly" repairs where a single link is snapped out and replaced in minutes.
Hygiene levels also differ drastically. Traditional belts can trap bacteria in fabric pores or seams, making them difficult to sanitize. The non-porous, injection-molded plastic of modular systems, combined with their open-grid options, allows for high-pressure wash-downs and complete sterilization, which is essential for FDA compliance.
Ultimately, while the initial investment in a modular system may be slightly higher, the total cost of ownership (TCO) is significantly lower. The extended service lifespan and the ability to perform preemptive maintenance make it the logically superior choice for any high-volume industrial operation.
Comparative Analysis of Modular 0.5" Pitch vs Traditional Conveying Systems
| Metric |
Traditional Belt |
Modular 0.5" Pitch |
Industrial Impact |
| Replacement Cost |
High (Full belt replacement) |
Low (Single module replacement) |
Reduced OPEX |
| Downtime Duration |
Hours to Days |
Minutes |
Higher OEE |
| Hygiene Level |
Moderate/Difficult to clean |
High/Easy Wash-down |
FDA Compliance |
| Product Stability |
Prone to slippage/stretching |
High Precision stability |
Less Product Waste |
| Service Lifespan |
Limited by overall wear |
Extended/Renewable |
Sustainable Asset |
| Installation |
Complex (Splicing/Tensioning) |
Simple (Snap-together) |
Faster Deployment |
FAQS
The small 0.5-inch pitch provides a highly stable and nearly continuous surface for components with small footprints. This prevents tiny electronic parts from tipping over or sliding during high-speed transport, ensuring they arrive at the assembly point in the correct orientation for robotic pick-and-place systems.
Yes, it is specifically designed for these environments. It is FDA-compliant and manufactured from materials like Polypropylene (PP) and Polyethylene (PE) that resist moisture and caustic sanitizing agents. The open modular structure also allows for easy drainage and deep cleaning to meet stringent food safety standards.
Unlike traditional belts that require a full replacement when a section is torn or worn, a modular system allows you to snap out a single broken module and replace it in minutes. This eliminates the need for costly full-belt replacements and drastically reduces production downtime, saving thousands in lost revenue.
Absolutely. The modular linked design is engineered for geometric flexibility. It can navigate curves, slopes, and inclines without compromising product stability. This allows designers to create more efficient, space-saving conveyor paths within a factory without risking product misalignment.
Polypropylene (PP) and Polyethylene (PE) offer the best overall chemical resistance, making them ideal for wash-down environments. However, if your application requires higher structural strength and lower friction for heavy-duty movement, Acetal (POM) is the preferred material choice.
The modules snap together using a tool-less assembly method, making integration fast and efficient. These belts are compatible with standard sprockets, side guards, and guide rails, allowing them to be easily integrated into most existing automated production lines with minimal modification.
Conclusion
The transition to a modular conveyor belt system, particularly the high-precision 0.5-inch pitch variety, represents a strategic upgrade for any modern manufacturing facility. By combining the durability of industrial-grade plastics like POM and PP with a maintainable, snap-together architecture, businesses can achieve a rare balance of high stability, stringent hygiene, and minimal downtime.
Looking forward, as Industry 4.0 continues to integrate smarter sensors and sustainable materials, the modular approach will only become more vital. We recommend that facility managers audit their current downtime costs and hygiene requirements to see where a modular transition could offer the highest ROI. To optimize your production line today, visit our website: www.rellwin.com.